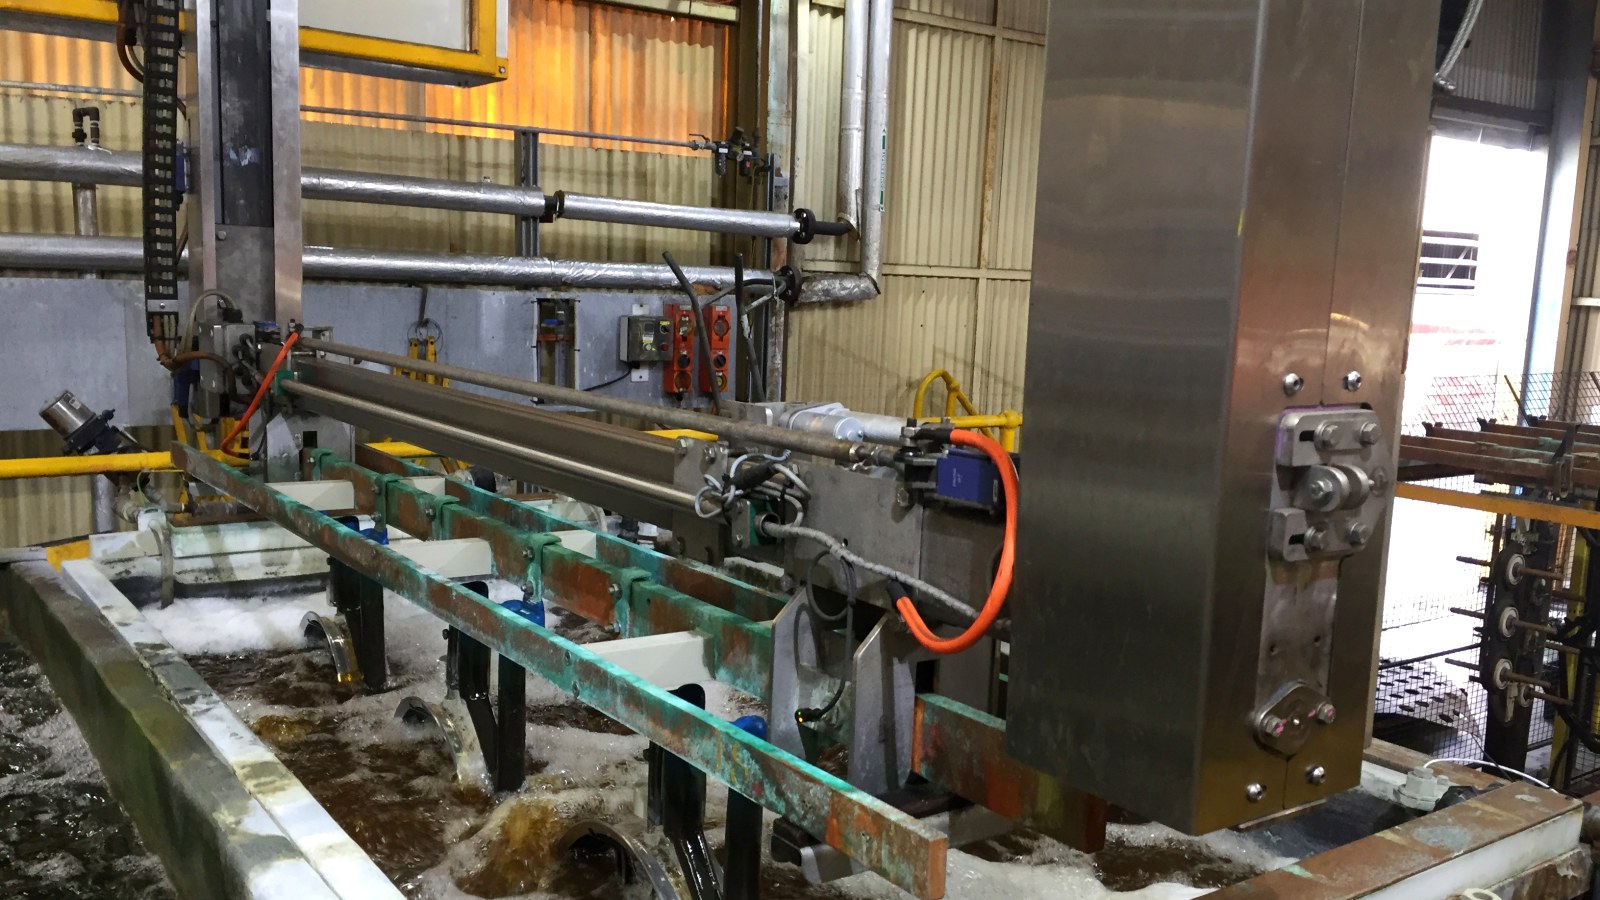
Cleaning Before Plating and Coating, Ultrasonic
Every finishing defect audit ends at the same place: the surface before the finish. Oils, buffing compound, oxide and handling soils survive dip degreasing — and reappear as adhesion failures, pits and rejects.
Misonics systems deliver finishing-grade cleanliness ahead of plating, anodising, painting and coating — with the endpoint defined and testable, not assumed.
What we remove in metal finishing & surface prep
Buffing & polishing compounds
Waxy abrasive residues packed into detail — the classic pre-plate failure.
Machining & stamping oils
Films that survive dip tanks and reappear under coatings.
Oxides & smut
On aluminium and steel ahead of anodising and plating.
Weld & heat scale
At joints where coating failure starts.
Handling soils
Fingerprints that become anodising stains.
Paint and coating removal, before and after
Coated and painted components photographed as received and after a documented cycle. Drag the handle across to compare.
Bearing housing hub. Housing bores are a fit, not a finish. Clean without touching the dimension.
Same trials, photographed separately
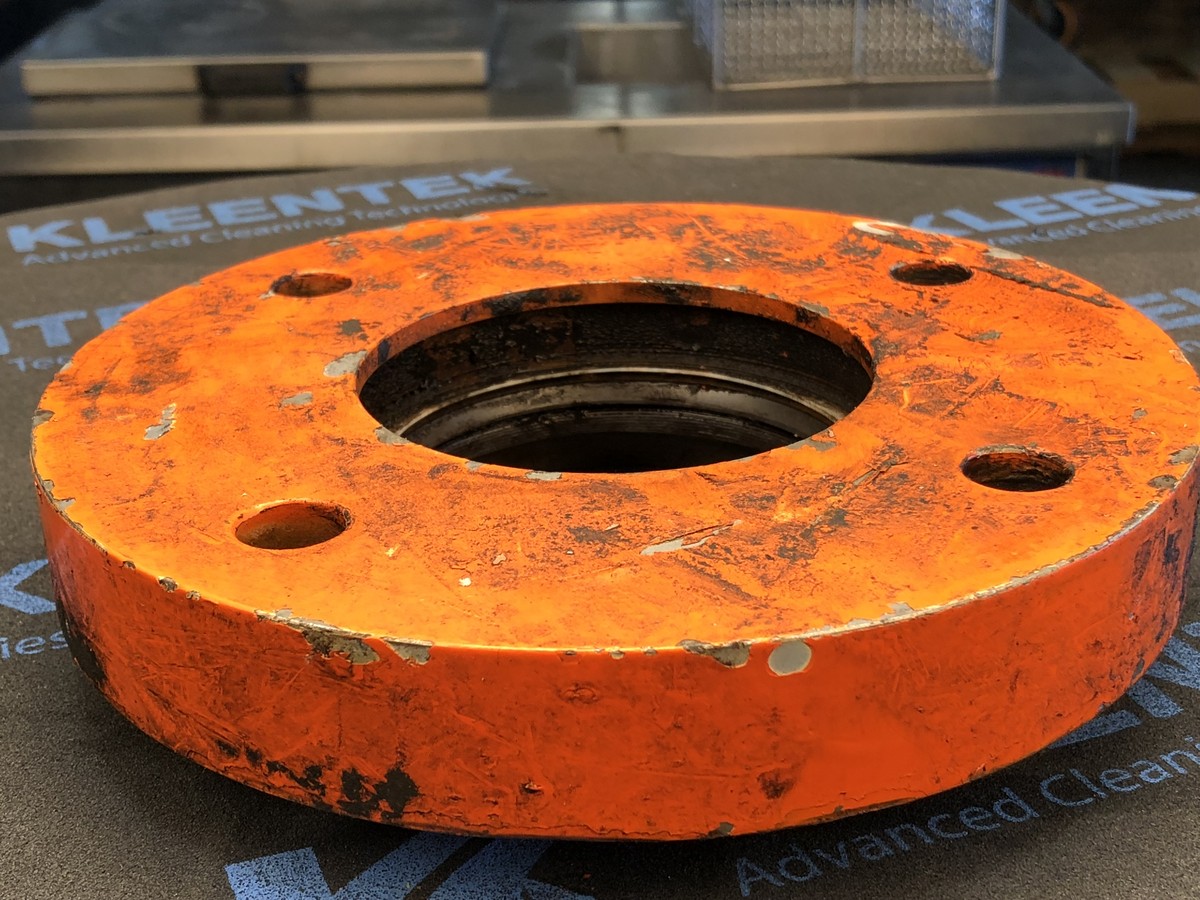
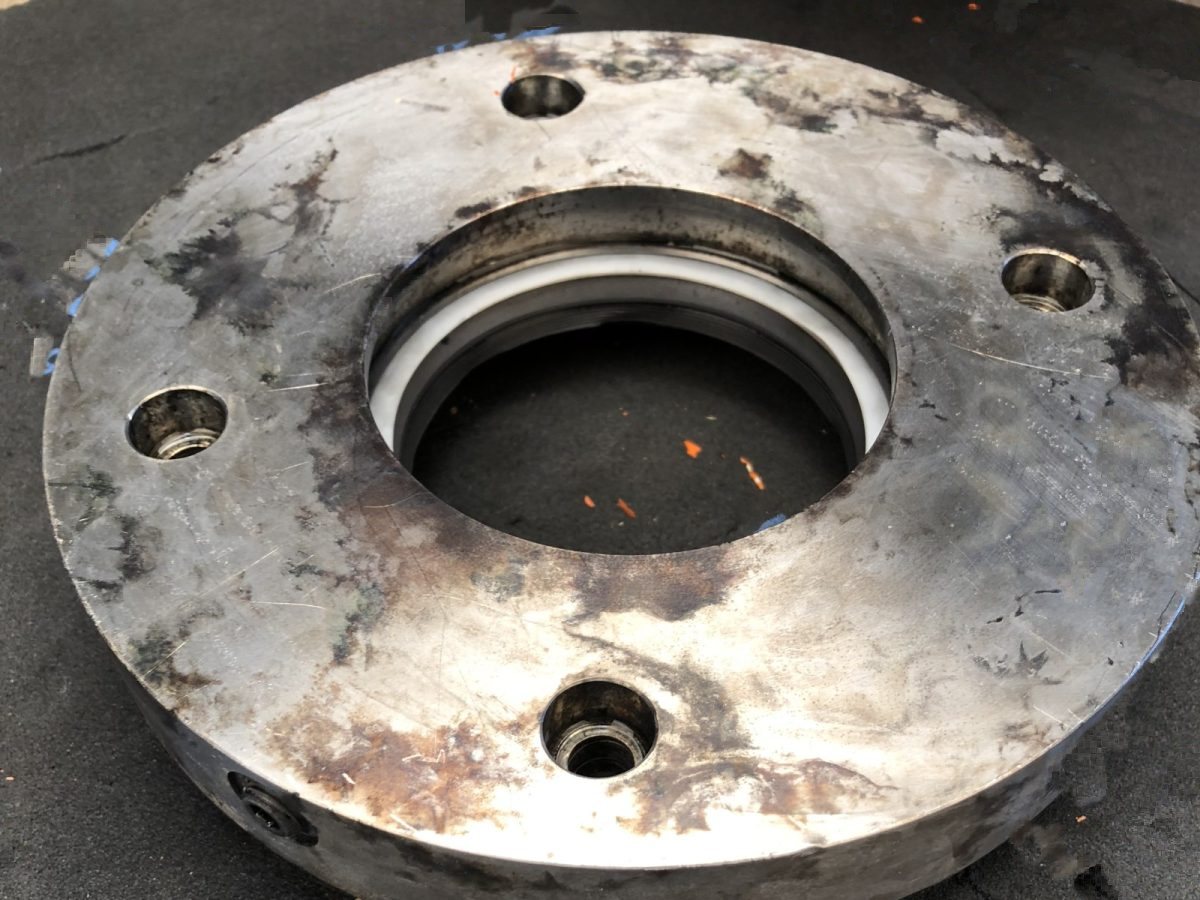
Painted flange plate. Coating off the whole plate, including the bore and the bolt holes, without blasting the substrate.
The finish is decided before the gun fires
Paint and powder do not fail in the film — they fail at the surface underneath it. Drawing compounds, machining oils, weld smoke, polishing pastes and handling residues are invisible at spray time and unmissable six months later: fisheyes, pinholes, poor flow-out and coatings that peel from the substrate. Solvent wiping moves contamination around; immersion ultrasonics removes it — from every face, hole and fold — to a condition you can test and record.
Pre-paint & pre-powder
Degrease, rinse and dry as a defined process step before phosphate, conversion coating or direct powder application.
The water-break standard
A cleaned surface holds an unbroken water film — a simple pass/fail test for paint-ready cleanliness on the shop floor.
Repeatable, recorded prep
Chemistry, concentration, temperature and cycle time are recorded parameters — every batch prepped the same way, shift after shift.
Real parts, real materials
Pre-plate
Components ahead of electroplating — compound and oil out of detail so the deposit bonds everywhere.
Pre-anodise
Aluminium ahead of anodising — uniform, stain-free surfaces into the tank line.
Pre-coat & pre-bond
Ahead of paint, powder and adhesive — where water-break-free is the entry ticket.
Cavitation cleans geometry it cannot see
Bubble collapse at the liquid–metal boundary lifts contamination from passages, galleries and cavities without anything touching the surface. Nothing abrades, nothing embeds, no metal is removed.
The VarioSonic G4 tracks the transducer array as temperature and load shift — conversion efficiency up to 95%.
Eliminates standing-wave hot and cold zones across a loaded basket.
Stored recipes and logged cycles — audit evidence produced as a by-product of running.
Multi-stage filtration and weir oil capture hold results steady as the bath loads.
Most faults identified — many resolved — without a site visit.
Heavy 316 stainless tanks, tested before despatch, every wearing part replaceable.
The machine follows the process
From manually loaded single-tank units to automated lines — and engineered systems where the catalogue ends.
Matched to the soil and the substrate
Pre-finish chemistry is matched to both soil and the finishing process downstream — free-rinsing formulations that leave nothing behind to interfere with deposition or adhesion.
Component coverage at a glance
| Component category | Specific parts / assemblies | Compatible materials |
|---|---|---|
| Pre-plate | Brass, zinc die-cast, steel parts | Substrate-specific chemistry |
| Pre-anodise | Aluminium components | Inhibited alkaline |
| Pre-paint | Fabrications, castings | Alkaline + rinse stages |
| Pre-bond | Assemblies, panels | Low-residue formulations |
| Rework | Stripped components | Per finishing system |
What are you cleaning?
Tell us what the part is, what comes off it, and what it has to pass. Technical sales will tell you whether ultrasonics is the right answer for that part and what it takes to run it on your own floor.
What metal finishing engineers ask us
Will parts pass a water-break test?
Can it remove buffing compound from detail?
Does it fit ahead of an existing tank line?
What rinse quality do we need?
Also in this sector
Manufacturing
In-process degreasing and pre-treatment cleaning across general fabrication and machining.
Automation & Robotics
End-effectors, precision actuators and component cleaning integrated into automated lines.
Molds, Castings & Foundry
Die and mould cleaning without dimensional loss — release agents, resin and scale.