A lock manufacturer needed machined brass lock bodies, casings and plugs critically clean before assembly — free of the swarf and oil that cause pins to stick, rejects to climb and finished locks to look second-hand. This is the documented trial process (T-3173) that solved it, stage by stage, with the photographs to prove it.
The contamination, understood before it was attacked
Nothing about this soil load is exotic — what makes it stubborn is how the three contaminants work together.
Fine brass swarf
Machining leaves a fog of fine brass chips and needles through every drilling, pin chamber and thread. In a lock, one retained needle is a mechanism that binds — this is functional contamination, not cosmetic.
Cutting oil — the binder
The oil film is what turns loose swarf into stuck swarf: it glues the fines to bores and casing walls, so air-blast and vibration can't shift them. Break the oil and the swarf loses its grip — which is why degreasing leads the process.
Machining pastes
Lapping and forming pastes don't blow off and don't rinse — they must be chemically dissolved or lifted from the surface they've bonded to. This is what sets the chemistry requirement: detergency plus surface-adhesion release, not just oil splitting.
The insight that shapes the whole process card: the swarf is not the problem — the oil holding it is. Dissolve the binder and paste load in a hot chemical stage, and the mechanical actions (spray, flood, rotation) can then evacuate the freed solids. Attack the swarf first and you're scrubbing glued chips.
The process: three stages to critically clean
| Parameter | Stage 1 — Hot degrease | Stage 2 — Rinse | Stage 3 — Dry |
|---|---|---|---|
| Action | Spray wash + injection flood wash (IFW), hot solution degrease | Identical spray + IFW mechanics, run on water | Hot air + vacuum |
| Medium | AquaVantage 1990 GD, 4.0% | Demineralised water | — |
| Temperature | 60 °C | 60 °C | 110 °C air |
| Filtration | 50 µm bag | 25 µm → 10 µm staged bags | — |
| Movement | Basket rotation, intermittent | Basket rotation | Rotation under airflow + vacuum |
Two details carry the result. The rinse deliberately repeats the wash mechanics with water — same spray, same injection flood through the bores — so anywhere chemistry reached, rinse water follows; nothing is left to dry into a pin chamber. And drying finishes with vacuum as well as hot air, because a blind hole holds its water against airflow alone; pulling the pressure down evacuates moisture from exactly the features that matter most in a lock. That combination — every stage reaching every feature — is what "critically clean" means in practice, and it is the difference between a part that is clean and a lock that works.
Before and after
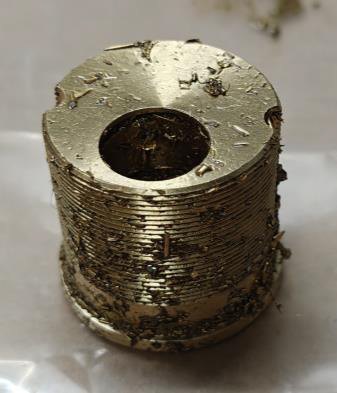
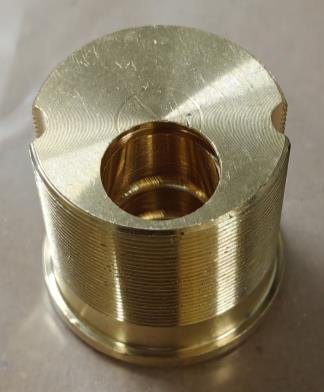
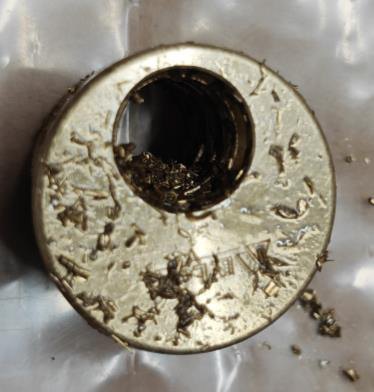
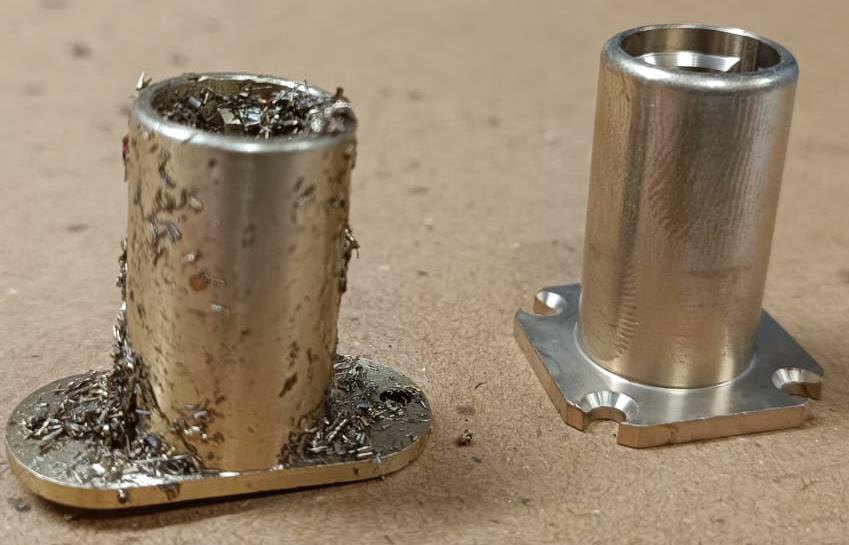
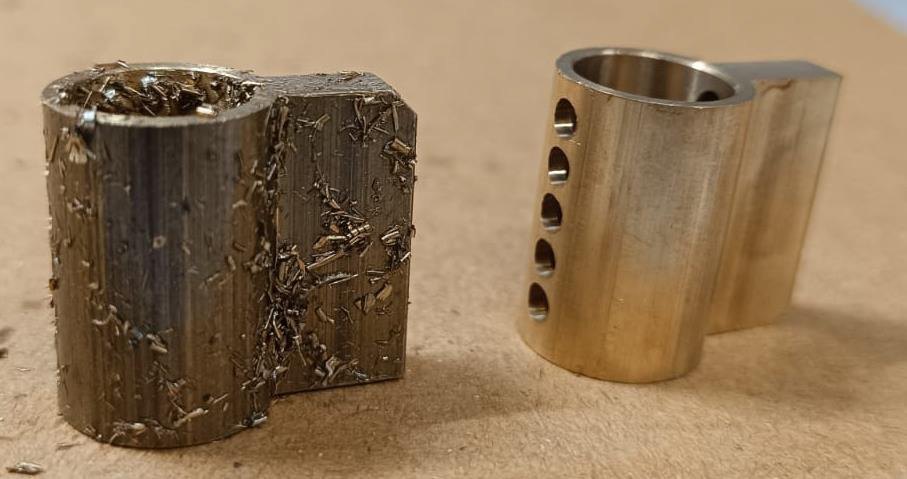
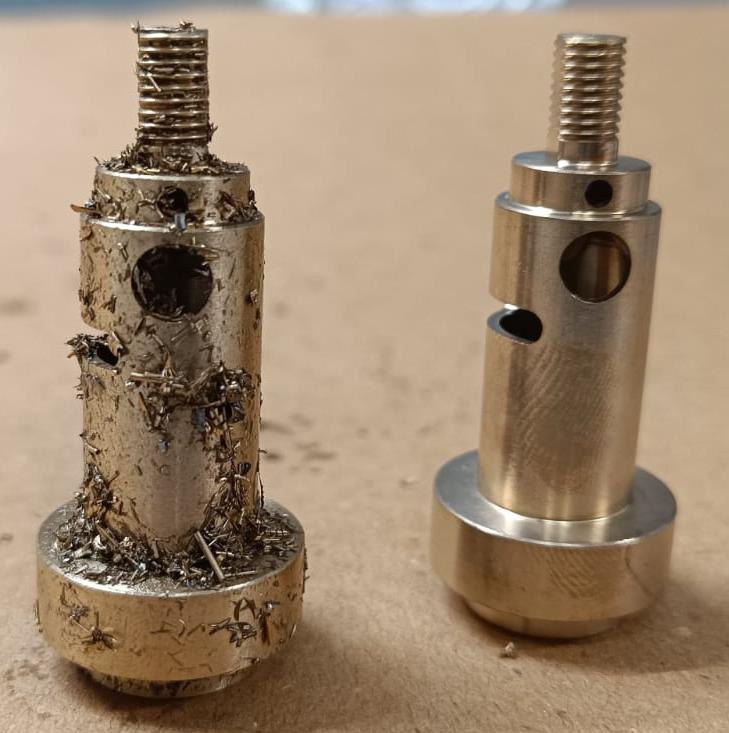
The results
The hardware and chemistry behind it
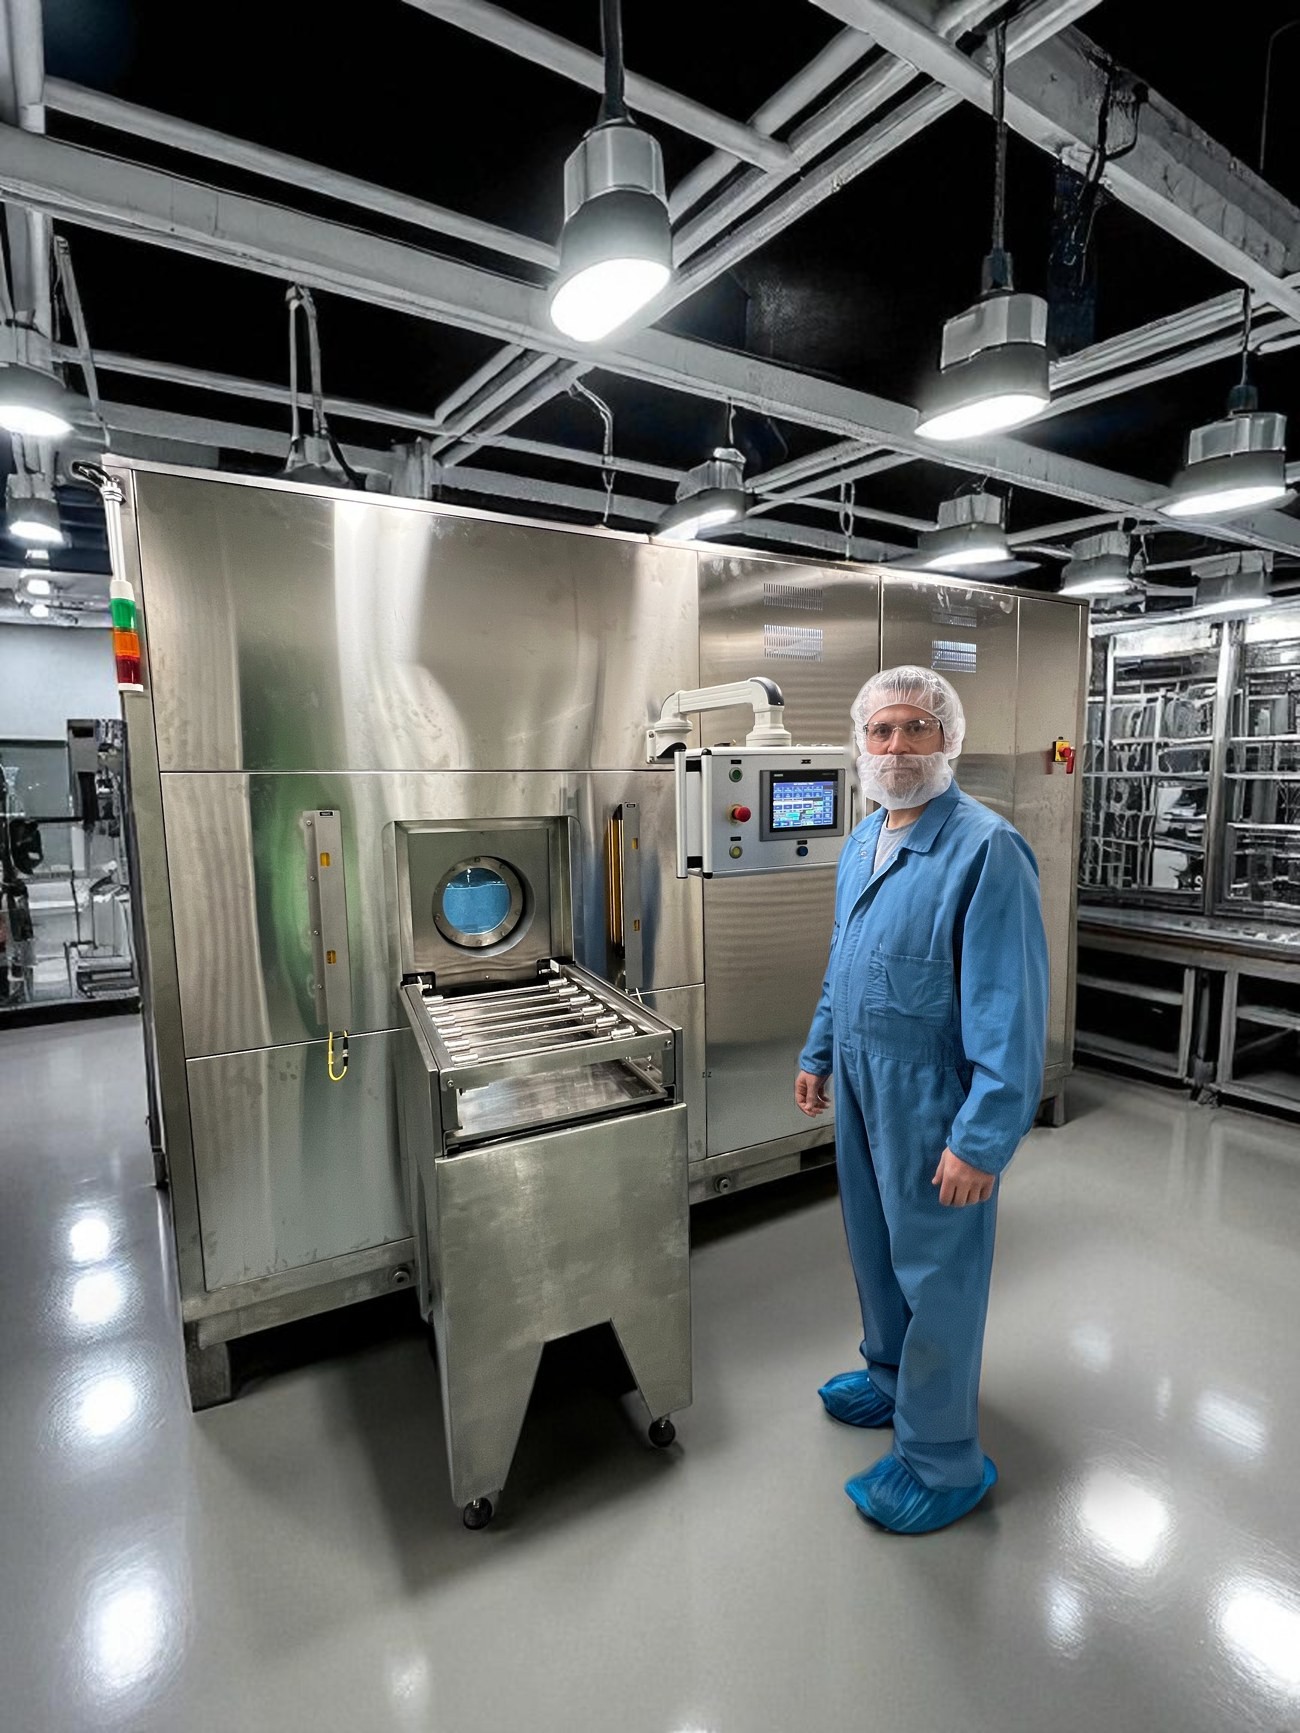
Misonics UltraWash — multi-stage cleaning system
Spray, injection flood wash, ultrasonics, rinse and hot-air/vacuum drying in one enclosed sequence, with basket rotation through every stage and staged filtration keeping removed contamination out of the process. Sized from cell to production line.
Explore the UltraWash range →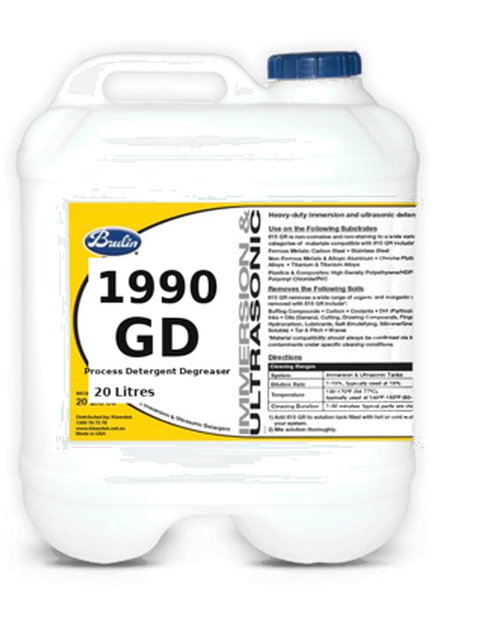
AquaVantage 1990 GD
Heavy-duty aqueous degreasing chemistry with the detergency to dissolve cutting oils and machining pastes and release bound swarf — free-rinsing, so nothing is left behind on a critically clean surface.
View the product, SDS and TDS →The process above started as a box of dirty parts and came back as a specification. Yours can too.
Questions about this process
What made brass lock bodies hard to clean?
What process cleaned them?
Is there proof?
Related: UltraWash multi-stage cell · Manufacturing parts cleaning · All case studies
What are you cleaning?
Tell us what the part is, what comes off it, and what it has to pass. Technical sales will tell you whether ultrasonics is the right answer for that part and what it takes to run it on your own floor.