Home / Insights / Case Studies
Insights · Case Studies

Diesel piston ring grooves: carbon out, dimensions untouched

Heavy coked carbon cleaned from a large-bore diesel ring belt in hot Brulin chemistry — with the grooves gauged unchanged afterwards.

6 min readBy Misonics application engineers

Ring-groove carbon is a dimensional problem wearing a cleaning costume: every mechanical method that removes the coke also removes or deforms metal the rebuild is required to keep. This documented application study cleaned the ring belt of a large-bore diesel piston in hot Brulin chemistry without anything touching the groove.

Industry
Engine rebuilding · mining · power gen
Component
Large-bore diesel piston, 3-groove ring belt
Contamination
Coked carbon · lubricant ash · oil film
Machine
Industrial ultrasonic tank, 25 kHz
Chemistry
AquaVantage 815 QR-NF, 10% v/v
Constraint
Zero dimensional change to grooves

The contamination

Coked carbon

Thermally polymerised in the ring belt over thousands of hours — insoluble in solvents, concrete-hard, and bonded into the groove roots where no tool reaches without contacting the flanks.

Lubricant ash

Mineral residue from burned oil packed behind the carbon banding — chemistry alone will not lift it; it needs cavitation working in place.

The dimensional trap

Scraping, wire-wheeling and blasting all remove or peen the groove flanks. A groove outside width or flatness spec scraps the piston — the cleaning method must be non-contact.

How these pistons were cleaned before

Soak for 24 to 72 hours

The pistons sat in a soak tank for one to three days to soften the oil and loose soil. The hard carbon in the ring belt stayed on.

Then sand or bead blast

The carbon came off by hand, with abrasive paper or in a bead blast cabinet. It takes a lot of operator time on every piston.

One slip scraps the piston

The skirts carry a coating. A moment's inattention at the blast cabinet takes the coating off or marks the grooves, and the piston is replaced with a new one at a cost of thousands of dollars.

The process

Process diagram
LOADparts in basketSTAGE 1 · DEGREASEOil & soot strip815 QR-NF · 10% v/v70 °C · sweep onsurface film removedSTAGE 2 · SOAK + SONICStaged ultrasoniccycles25 kHz immersioncarbon undercut & liftedinter-cycle filtrationSTAGE 3 · RINSEHot rinsechemistry clearedfrom groove rootsSTAGE 4 · DRY + GAUGEDry & verifygroove width, depth,flank flatness gaugedRESULTverified & loggedSweep on throughout — even attack along the full circumference; filtration between cycles takes removed carbon out of the bath.
ParameterValue
ChemistryAquaVantage 815 QR-NF at 10% v/v
Temperature70 °C
Frequency25 kHz, sweep
CycleStaged cycles with inter-cycle filtration
VerificationGroove width, depth and flank flatness gauged against drawing after cleaning

Before, during, after

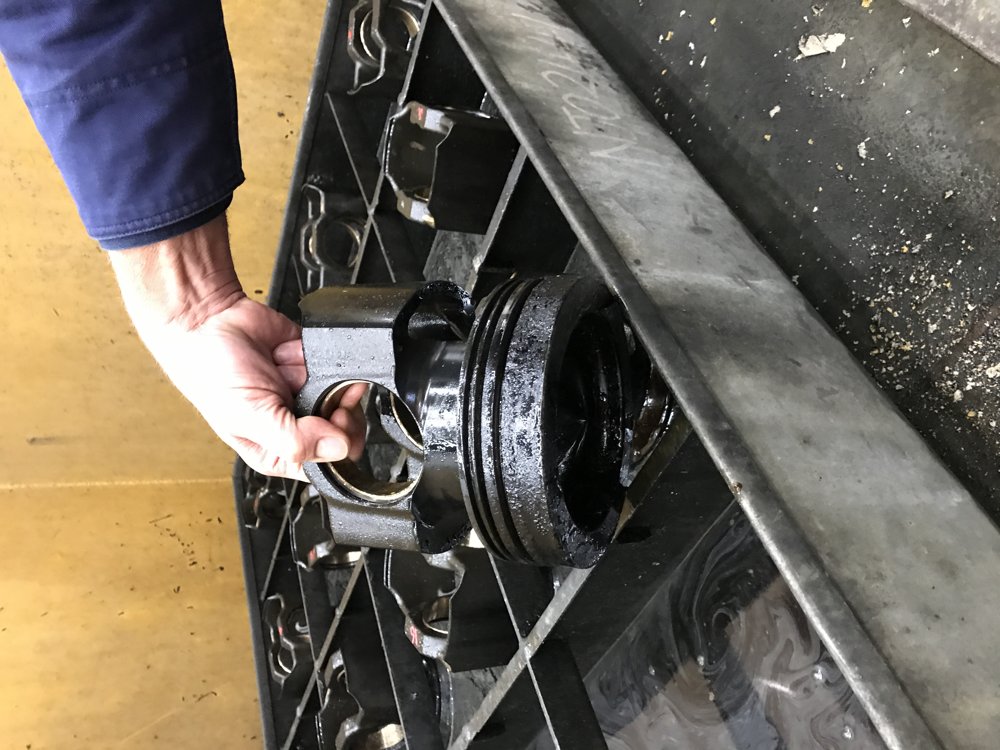
Pistons in the soak tray, as they came off the engine.
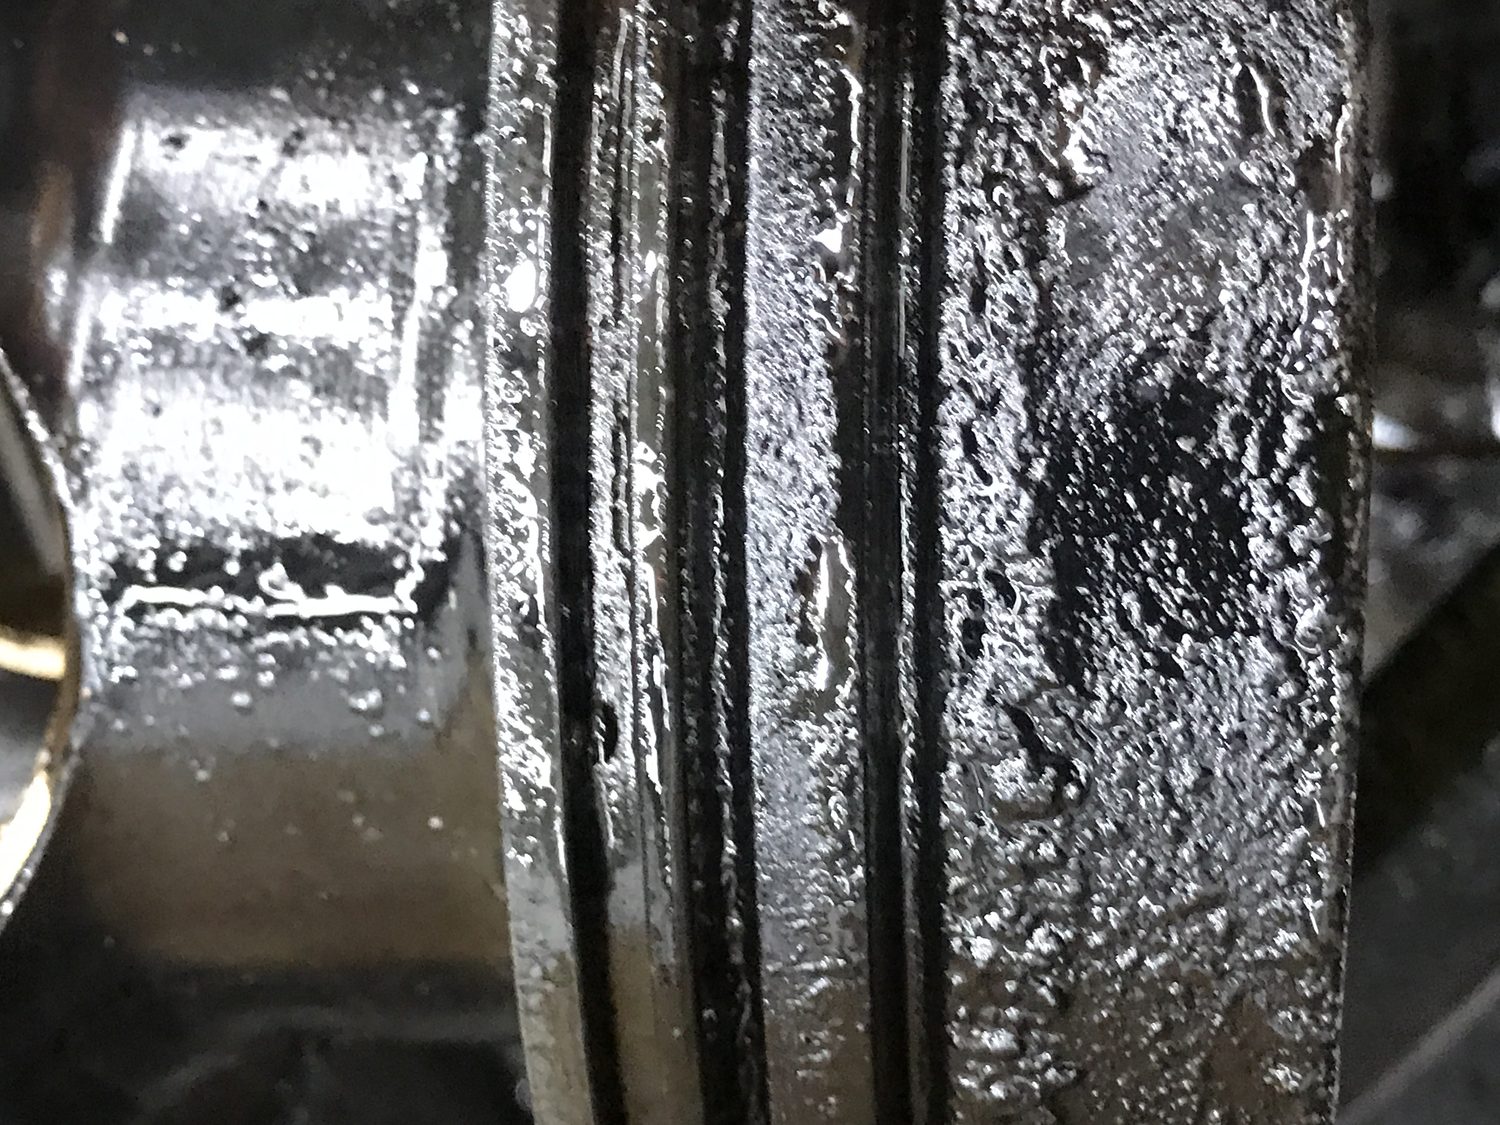
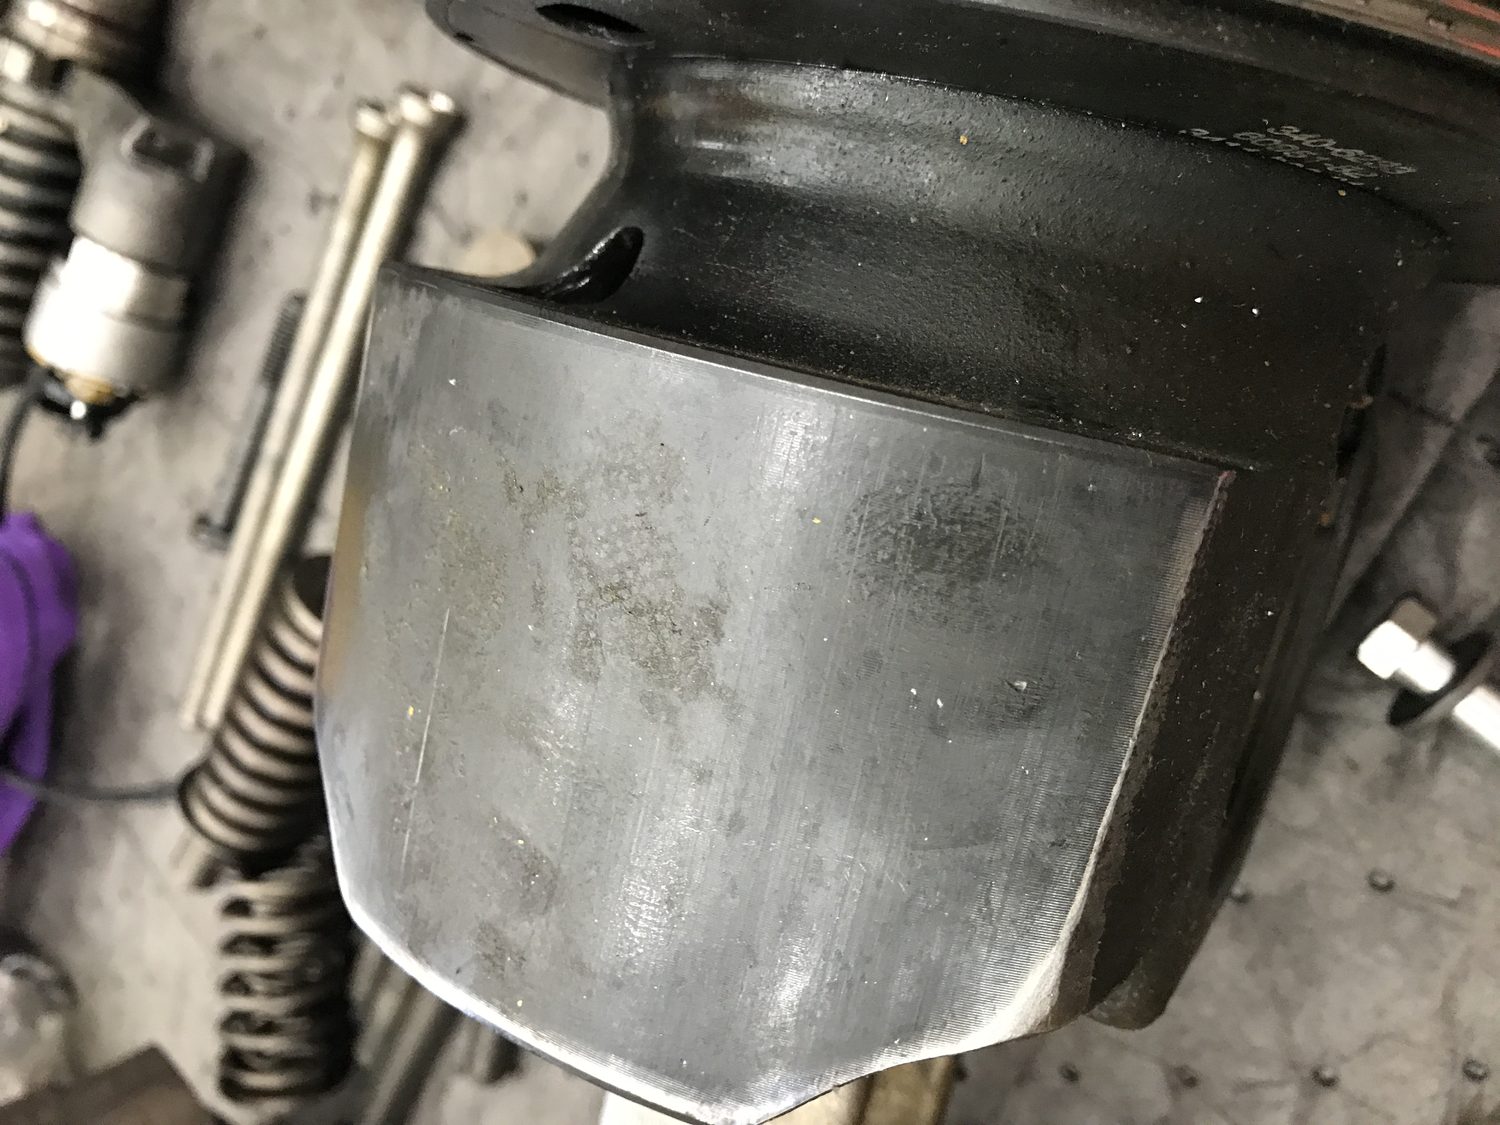
Before: hard carbon on the ring belt and in the grooves.
Before: the skirt under oil and carbon.
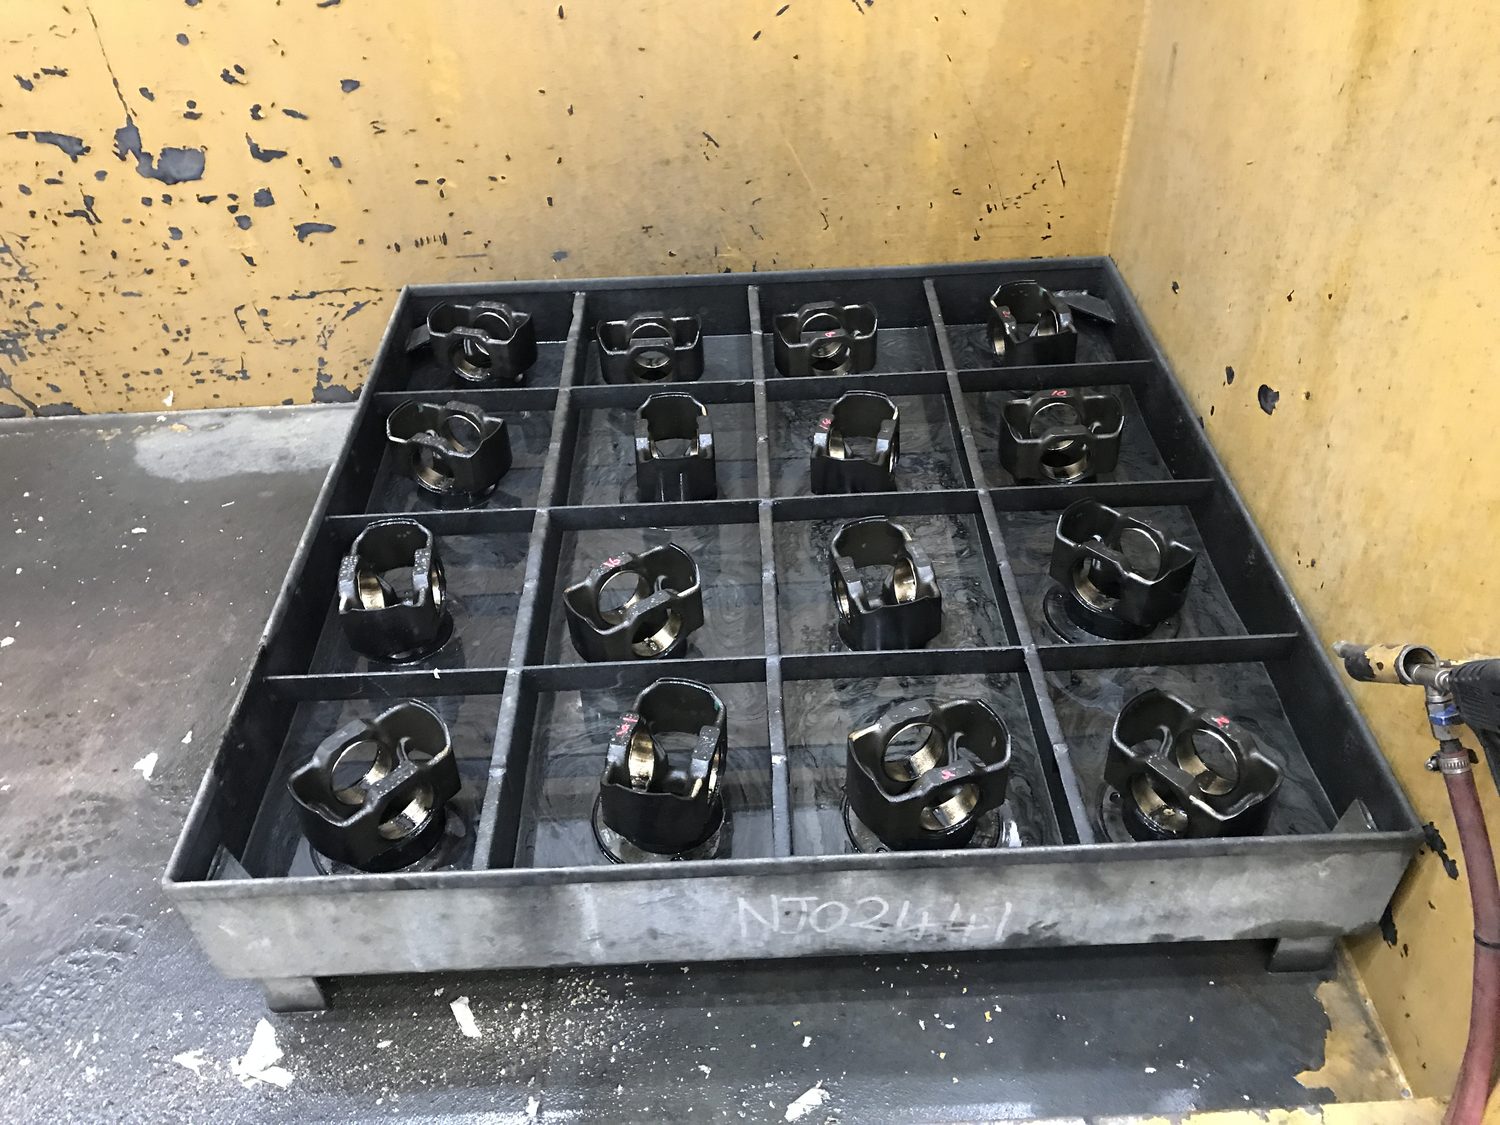
A full set racked in the tray.
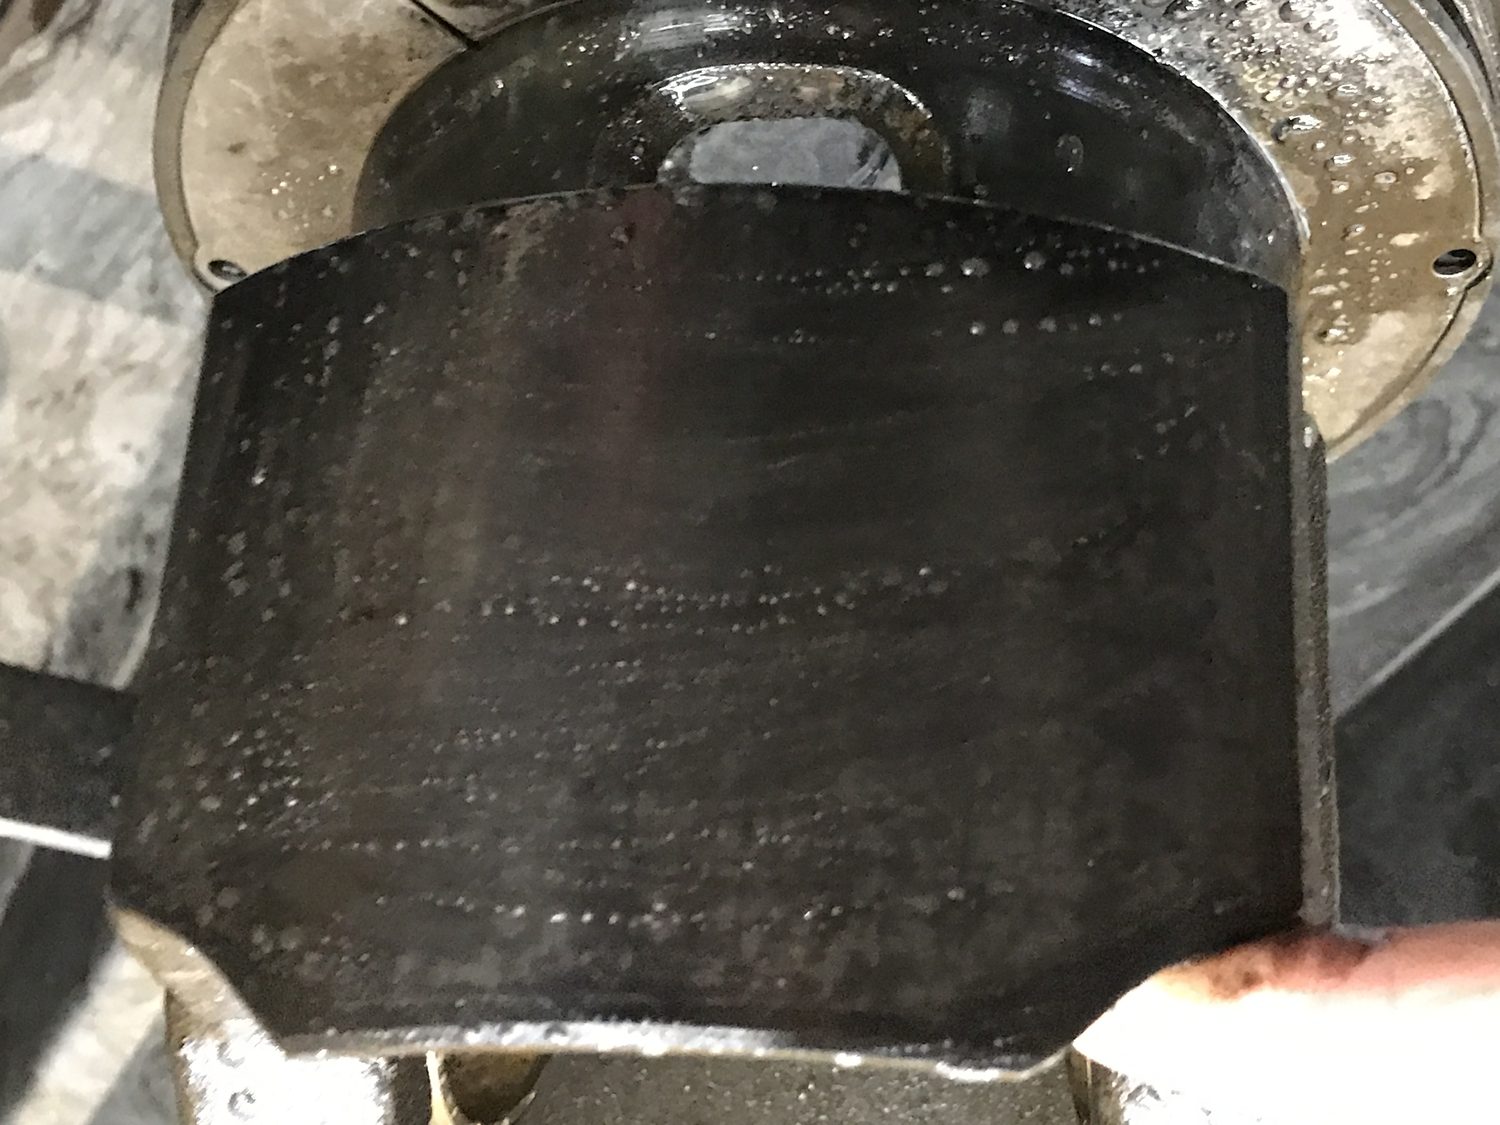
After: the skirt clean, machining marks visible.
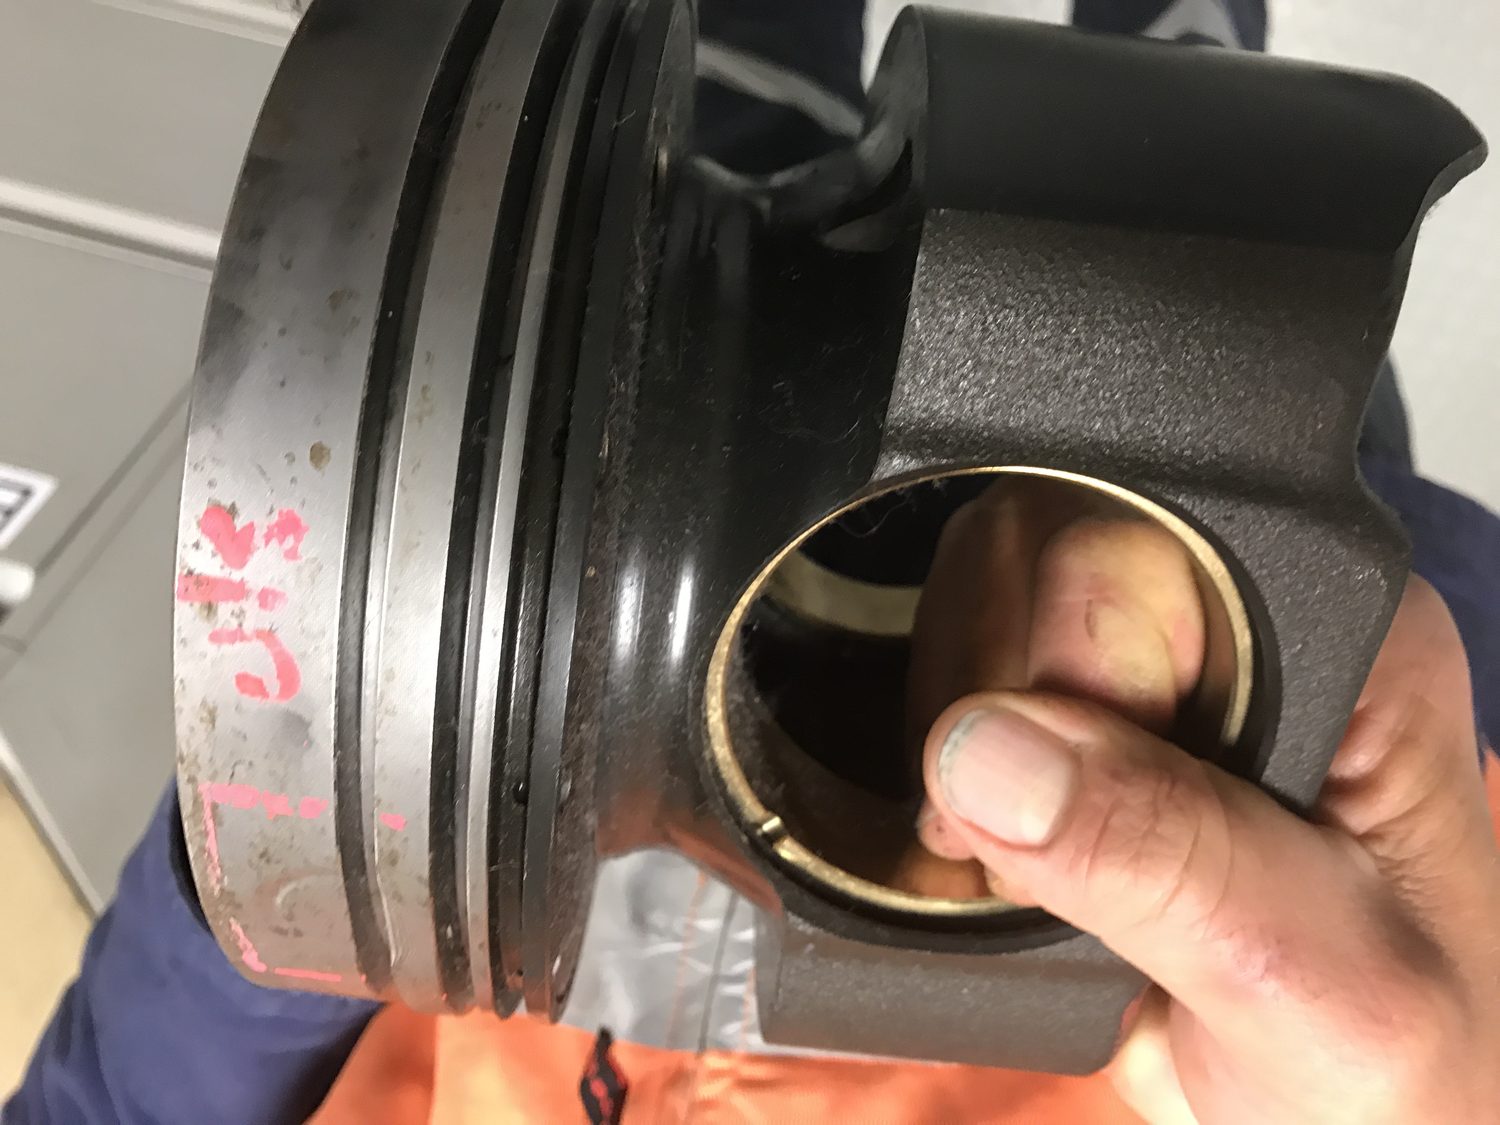
After: grooves and gudgeon bush clean, the dark skirt coating still in place.

The results

Grooves clean to the root. Carbon and ash removed from all three grooves and the banding below — including the corners mechanical methods cannot enter.
Dimensions untouched. Groove width, depth and flank flatness gauged unchanged — the entire argument for the method.
No embedded media, no peening. Nothing was blasted, scraped or wheeled; downstream seating and blow-by behaviour is protected.
A written, repeatable card. Chemistry, concentration, temperature, frequency and staging documented for every future piston.

Hardware and chemistry

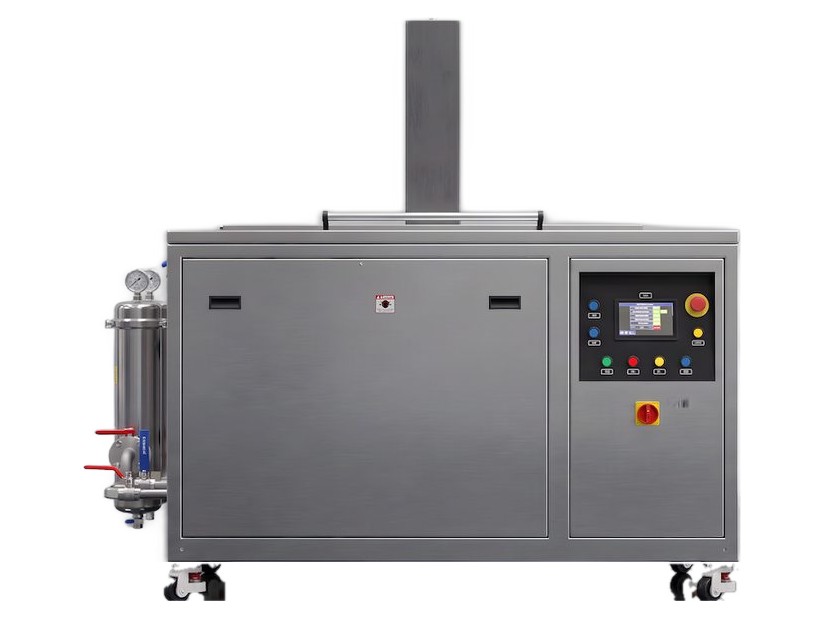
Heavy-duty industrial ultrasonic tank

Heavy-duty industrial ultrasonic tank

25 kHz with sweep, heated to 70 °C, weir and bag filtration keeping removed carbon out of the bath. Sized to the largest piston in the rebuild program.

Talk to us about tank sizing →
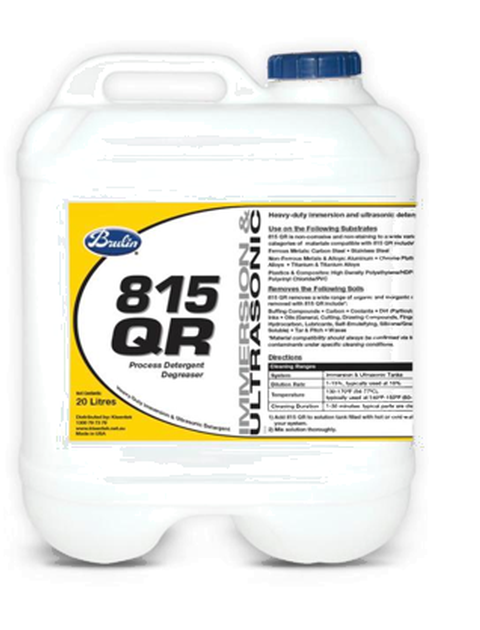
AquaVantage 815 QR-NF, 20 litre

AquaVantage 815 QR-NF

The MRO-grade carbon remover in the AquaVantage range — formulated for baked and coked soils on rebuild work, free-rinsing, with corrosion inhibition.

View the product, SDS and TDS →
The trial is the product. This study is the process card a rebuild shop runs on every piston — and the same trial-first sequence applies to your parts. Send them; the card comes back with your numbers on it.
FAQ

Questions about this process

Why not scrape or blast the grooves?
Every mechanical method that removes the coke also removes or peens the groove flanks. A groove outside width or flatness spec scraps the piston, so the method has to be non-contact.
What chemistry and settings?
AquaVantage 815 QR-NF at 10 percent, 70 degrees C, then staged ultrasonic cycles at 25 kHz with filtration between cycles, a hot rinse and a dry.
What about the dimensions?
The grooves were gauged after cleaning and were unchanged: width, depth and flatness all within specification.

Related: MSX floor-standing tanks · Engine rebuild parts cleaning · Parts washers compared · Ultrasonic parts cleaners · All case studies

What are you cleaning?

Tell us what the part is, what comes off it, and what it has to pass. Technical sales will tell you whether ultrasonics is the right answer for that part and what it takes to run it on your own floor.

Talk to an engineerMore Insights