Joint design:
where welds are won or lost.
Energy director dimensions, the four joint types and when to use each, near-field against far-field — the decisions that must be made before the mould tool is cut.
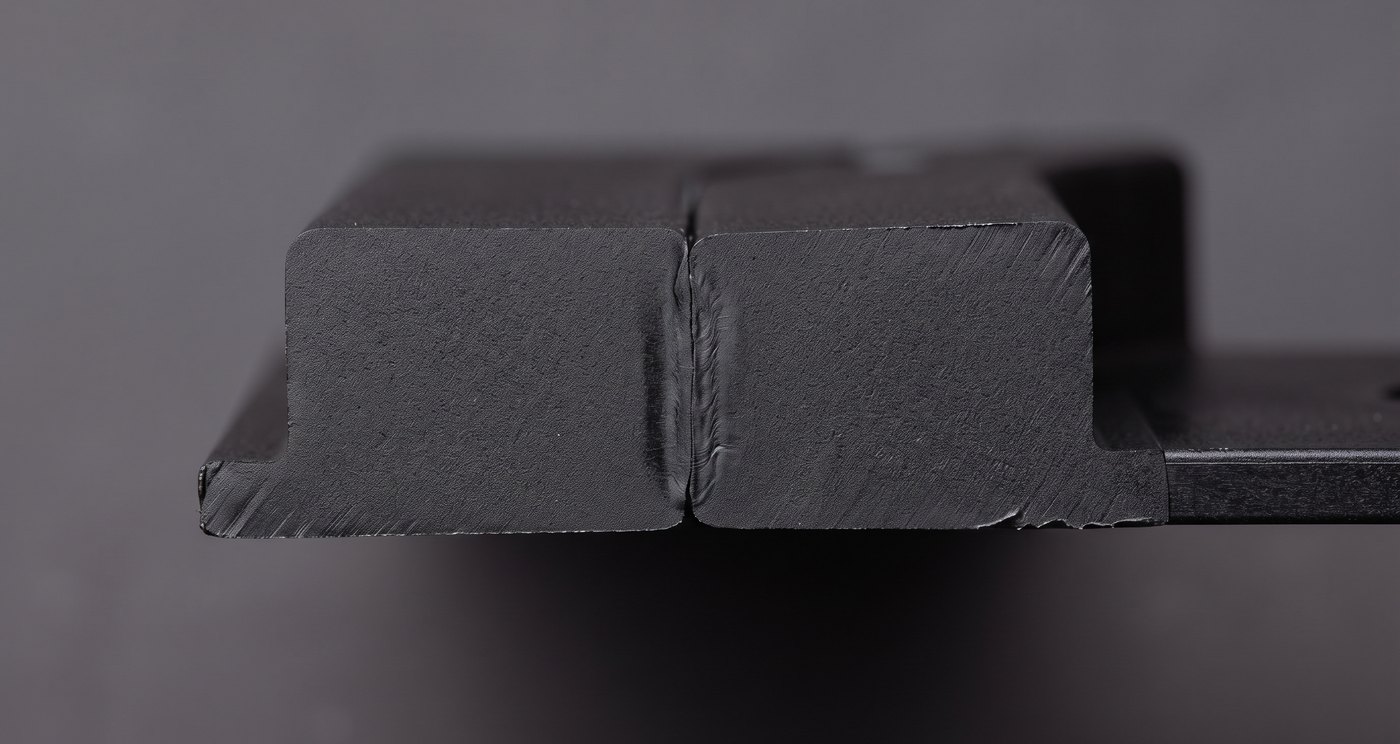
Almost every ultrasonic welding problem we are asked about is a joint design problem being attacked with machine settings. Get the joint right and the weld is easy on any decent machine. Get it wrong and no amount of amplitude will rescue it.
The energy director
A flat face butted against another flat face does not weld well — the energy spreads across the whole area and nothing gets hot enough. An energy director is a small triangular ridge moulded onto one half of the joint. It concentrates all the ultrasonic energy into its apex, which melts first and then flows out to fill the joint.
| Feature | Dimension | Why |
|---|---|---|
| Height | 0.3 to 0.7 mm (0.01–0.04 in) | Enough melt volume to fill the joint without excessive collapse |
| Base width | No more than 20–25% of wall thickness | Wider than that and the energy is no longer concentrated |
| Included angle — amorphous | 90° (ABS, PS, PC, acrylic) | Amorphous resins soften over a range; a broader apex suits them |
| Included angle — semi-crystalline | 60° (nylon, PP, PE, acetal) | Sharp melting point needs a finer point to concentrate energy harder |
The four joint types
| Joint | Best for | Minimum wall | Notes |
|---|---|---|---|
| Butt with energy director | General purpose, easiest to mould | Standard | Simplest and cheapest. No self-location, so tooling has to hold alignment. Flash visible. |
| Step joint | Mechanical strength with better cosmetics | 1.6 mm (0.062 in) | Self-locating, stronger than butt, tolerant of moulding variation. Hides flash on one side. |
| Tongue and groove | Hermetic seals, medical devices | 2.3 mm (0.09 in) | Greatest strength potential. Hides flash inside and out. Hardest to mould — needs tight tolerances. |
| Shear joint | Hermetic seals in semi-crystalline resins | Thinner walls acceptable | Parts telescope together as the edge melts, so the melt never sees air. The answer for nylon and PP. |
Shear joint dimensions
Weld depth should be 1.25 to 1.5 times the wall thickness to approach parent-material strength. The interference between the two halves is what does the work — too little and it will not seal, too much and you overload the machine and mark the parts.
Near field or far field
This is about where the horn touches the part relative to the joint.
- Near field — horn contact within 6 mm (0.25 in) of the joint. Shorter weld times, lower energy, more consistent. Design for this whenever you can.
- Far field — horn contact further than 6 mm from the joint. The energy has to travel through the part to reach the weld, so you need higher amplitude and longer weld times. Workable in rigid amorphous resins; difficult to impossible in soft semi-crystalline ones.
Other design rules that matter
- Minimum wall 1.5 mm. Below about 1.5 mm (0.06 in) the wall behaves like a spring and absorbs the energy instead of passing it to the joint.
- Radius every internal corner. A sharp 90° internal corner is a stress concentration, and under ultrasonic vibration it will crack.
- Support the joint from below. The fixture must back up the weld line. An unsupported joint flexes and the energy goes into movement rather than melt.
- Keep it flat and level. Any twist between horn face and joint gives you an uneven weld across the part.
- Size limit. A single continuous weld is practical up to roughly a 250–300 mm square footprint, material depending. Beyond that, expect multiple horns or a different process.
- Design a flash trap if cosmetics matter. Molten material has to go somewhere — give it a designed void rather than letting it squeeze out where it shows.
Do this before the mould tool is cut
All of the above is cheap to change in CAD and expensive to change in steel. Send the part model and we will have the joint reviewed by application engineers who weld for a living — before the tool exists, not after the first shots fail.
What are you welding?
Ultrasonic welding is decided by the parts — the resin, the wall, the joint and what the weld has to do. Send photos and drawings through the enquiry form and you get an engineered answer.